Test inks
Surface energy measurement
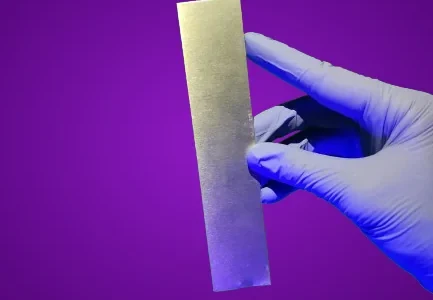
In a few seconds, the ink tells you whether the surface is ready to bond, paint or print. Before the step, not after the customer complaint.
22 – 72 mN/m
Measuring range, both ranges
ISO 8296: 2003
Standard, extended range
ASTM D2578-09
Standard, non-toxic range
Bottle or marker
Formats available
- Reply within 48 h from an expert
- Trials in our laboratory in Québec City
- Quote with no commitment
Technical datasheet, 2 pages, PDF
Dimensioned footprint, required utilities, protocols. To pass on to your integrator.
Know before, not after
Before bonding, painting or printing
The line spreads: the surface is ready. It pulls into droplets: the next step will fail.
To monitor production
On witness parts, the reading shows the treatment stays stable from part to part.
For a quality file
It is measured proof, backed by a standard, that an auditor can check.
See also
One line of ink, one value
Each ink matches a known value. If the line spreads, the surface is above it. If it beads, the surface is below. Trying several inks brackets the real value.
Two ranges: the extended range (ISO 8296: 2003) for all materials, the non-toxic range (ASTM D2578-09) for PTFE, EPDM, PET and PVC.
Technical specifications
Installation at your site
Indicative values, confirmed during the study of your process.
- Floor footprint
- [x] mm
- Mass of the assembly
- [y] kg
- Extraction required
- [z] m³/h
- Protocols available
- [x]
- Cable lengths
- 3, 5 or 7 m
- Indicative lead time
- [y] weeks
Maintenance, consumables and warranty
- Electrode service life
- [y] h
- Replacement cost
- [z] $
- Preventive maintenance
- [x]
- Warranty
- [y]
- Rental possible
- yes
Frequently asked questions
How do I know whether this equipment suits my part?
Send us the part. We treat it in our Québec City laboratory. Within 48 hours you get the surface energy before and after, the settings used, and a frank opinion if plasma is not the right answer.
Has my material already been treated?
Materials qualified in the laboratory: [x]. Yours is not listed? That is the most common case. Send us three samples: a measured answer within 48 hours.
Can it be rented before buying?
Yes. You test the equipment on site, with your parts and your operators, before investing. Terms: [x].
What documents do you provide for a customer audit?
The process file: plasma settings, measurement methods, results on your parts and procedures. For regulated markets, it follows your sector's requirements.
And if no configuration fits?
We then design a custom reactor, matched to your material and your throughput. See the custom reactors →
To compare, or to complete
 Precise area
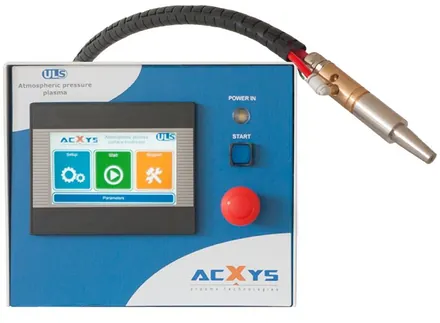
Compact torch
A nozzle that blows plasma straight onto the area to be treated, a few millimetres from the part. The most common way to activate a precise area.
View the page → Powders and granulatesSpecialised stations
Some materials cannot be treated like a part: a powder requires every grain to pass through the plasma, in line and with no manual intervention.
View the page →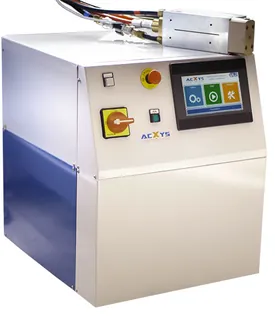 Wide web
Plasma curtain
A continuous curtain across a full width, for panels, sheets or webs on the move. Seven working widths from 60 to 500 mm.
View the page →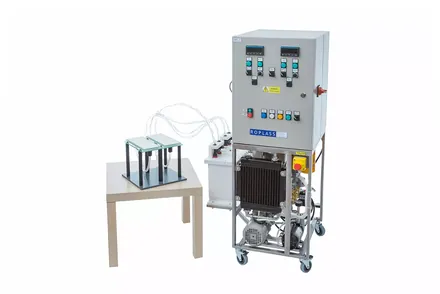 Whole surface
Surface source
A discharge spread across the whole electrode, treating flat parts and flexible films uniformly. No sweeping, so no over-treated band.
View the page →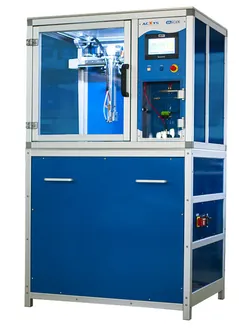 Automated station
Turnkey cell
An enclosed cell with a Cartesian robot, plasma source and safety interlocks. You program a path, the station replays it identically.
View the page →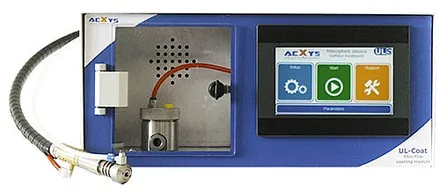 Film deposition
Deposition station
When activating is no longer enough: a 1 to 300 nm functional film deposited by atmospheric plasma, anti-corrosion or anti-scratch depending on the precursor.
View the page → To specification
DBD reactor
No catalogue configuration fits? Our experts design the reactor to your specification, dimensions and gases included.
View the page →As seen in